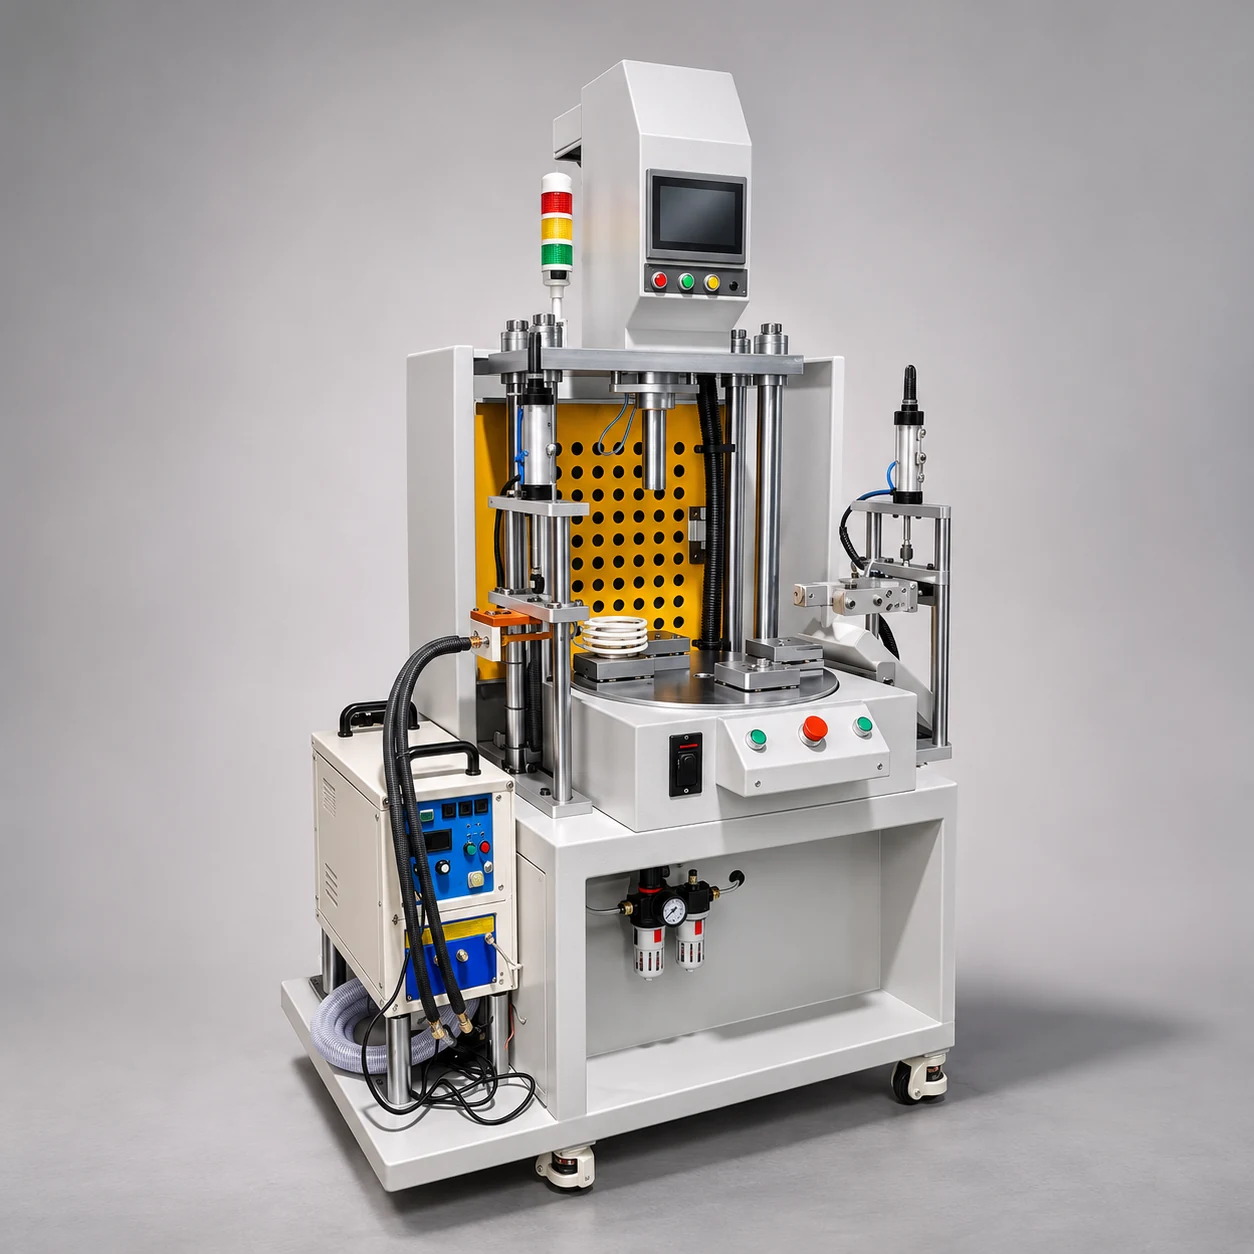
An OK/NG indication is useful only when the underlying acceptance rules are validated. Product specifications and process-control windows serve different purposes and must be linked through representative testing.
Define checks by process stage
- Before motion: correct recipe, part ID and presence detection
- During pressing: contact point, force limits, travel bands and curve windows
- After motion: final depth, hold time and functional acceptance checks
- After a fault: NG separation, lockout, reset permissions and disposal records
- During maintenance: sensor calibration, fixture baselines and controlled fault tests
Collecting a curve on every cycle does not prove that every possible defect can be detected. Detection-rate claims require appropriately designed tests and statistical evidence. Coordinate acceptance thresholds with the customer’s product drawing and quality requirements.
This article is general engineering guidance. Machine functions, performance and acceptance criteria must be confirmed against representative samples and the specific project agreement.
Discuss an application with BRUNSK. You may share appropriate drawings, materials, target force, stroke, cycle time and inspection requirements.